
Product Categories
- Atom Cutter Cutting Knives Knife Blades For Sale
- Axyz Cutter Cutting Knives Knife Blades For Sale
- Aristo Cutter Cutting Knives Knife Blades For Sale
- Blackman & White Cnc Knives Knife Blades For Sale
- Bullmer Cutter Cutting Knives Knife Blades
- Colex Cutter Cutting Knives Knife Blades For Sale
- Colex Milling & Router Bits For Sale Shop Online
- Comelz Cutter Cutting Knives Knife Blades For Sale
- Comagrav Cnc Knives Knife Blades For Sale Shop
- Esko Kongsberg End Mill Cutters And Router Bits
- Esko Kongsberg Cutter Cutting Knives Knife Blades
- Eastman Cnc Knives Knife Blades For Sale Shop
- Ecocam Tangential Knives Knife Blades For Sale
- Elitron Cnc Knives Knife Blades For Sale Shop
- Fk Group Cnc Knives Knife Blade For Sale Shop
- Filiz Cnc Knives Knife Blade For Sale Shop
- Gerber Cutter Cutting Knives Knife Blades For Sale
- Humantec Cnc Knives Knife Blade For Sale Shop
- Investronica Cnc Knives Knife Blade For Sale Shop
- Iecho Cnc Knives Knife Blades For Sale Shop Replac
- JingWei JWei Cnc Knives Knife Blades For Sale Shop
- Kawakami Cnc Knives Knife Blade For Sale Shop
- Kuris Cnc Knives Knife Blades For Sale Shop
- Lectra Cnc Knives Knife Blades For Sale Shop
- Multicam Cutter Knives Cutting Knife Blades
- Mimaki Cnc Knives And Plotter Cutter Knife Blades
- RuiZhou Cnc Knives Knife Blades For Sale Shop
- Ronchini Cnc Knives Knife Blades For Sale Shop
- Summa Cutter Cutting Knives Knife Blades For Sale
- Summa End Mill Cutters And Router Bits
- Talamoni Cnc Knives Knife Blade For Sale Shop
- Teseo Cnc Knives Knife Blades For Sale Shop
- Wild Cnc Knives Knife Blade For Sale Shop
- Zund Cutter Cutting Knives Knife Blades For Sale
- Zund End Mill Cutters And Router Bits
- Other Tungsten Carbide Cutting Knives Knife Blades
- Protek Cnc Knives Knife Blades For Sale Shop
- Vinyl Cutter Blades,Plotter Cutting Blades Sale
- Other Cloth Cutting Knife Blades For Sale Shop
- Aluminum End Mill Cnc Router Tools Cutter Bits
- Milling Router Bits Routing Cutters For Sale Shop
- Tungsten Carbide Digital Vinyl Cutter Knife Blades
- Textile Blades,Textile Knives,Non-woven Cutters
- Notching & Punching Tools For Sale Shop
- Paper Cutting Knives Knife Blade For Sale Shop
- Carbide reversible knives,Replacement Tip Turnover
- Conveyor Belts Cutting Underlay Felt Pad For Sale
- Sharpening Disk Grinding Wheels Stones Drums Sale
- Knife for Button Hole Machine,Button Hole Knives
- Valiani Cnc Knives Knife Blades For Sale Shop
- Flatbed Digital Cutting System Tools Accessories
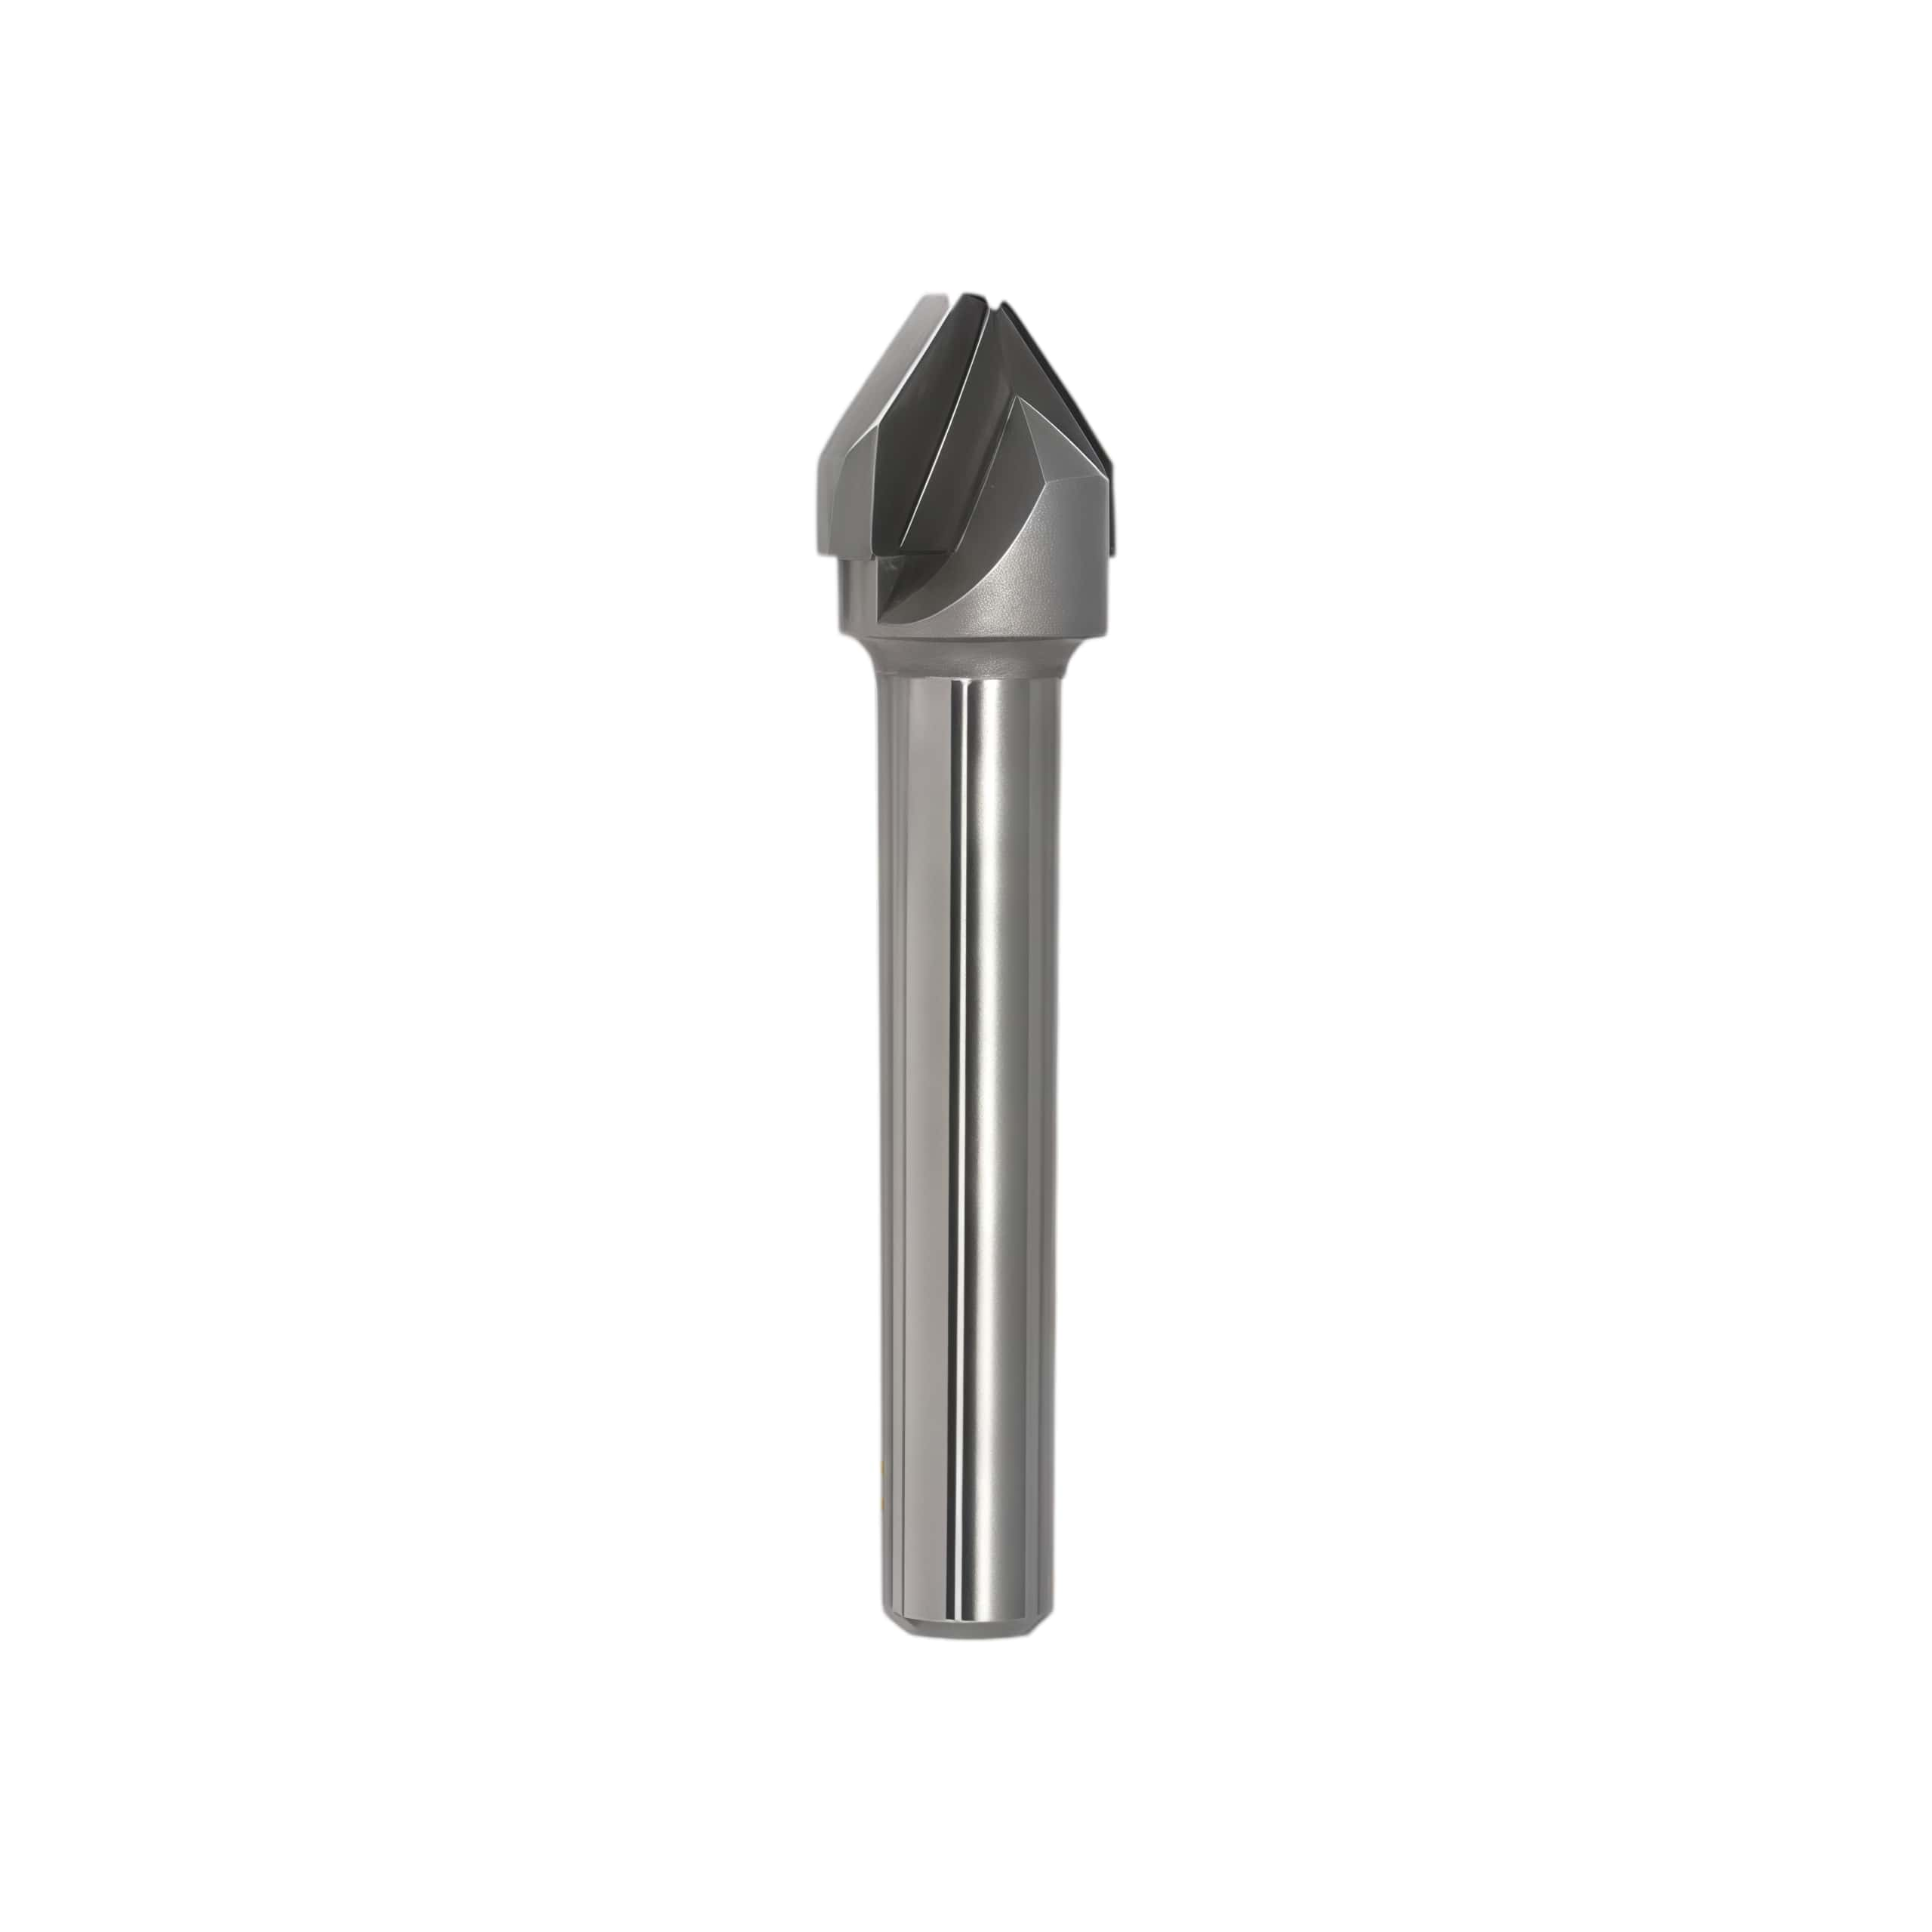


These tools are engineered with a flat tip (flat-bottom landing) to score through the top aluminum skin and polyethylene (PE) or mineral core while leaving the bottom aluminum skin intact (~0.2 mm–0.4 mm of core) for clean, crisp box/tray bending without cracking the outer skin.
OEM & Compatible Folding Bit Part Numbers Breakdown
| Part Number / Code | Tool Type & Geometry | Shank & Angle Specs | Core Function & Application |
| 95-00047-37-72 | 90° V-Groove Folding Bit | 90° Included Angle | MultiCam OEM spec 90° V-groove bit for standard 90-degree right-angle architectural box & tray folds in ACM/Dibond/Alucobond. |
| 000419-99168 | Carbide Tipped Folding Tool | Heavy-Duty Carbide Tip | Brazed carbide-tipped folding tool engineered for high-wear abrasive mineral-core ACM panels (e.g., Fire-Retardant FR-core Alucobond). |
| 000419-99167 | 90° Folding Tool | 90° Solid/Tipped Geometry | Standard 90° ACM score-and-fold router bit for standard PE-core composite panels. |
| 95-00047-37-71 | 90° Folding Tool (37-71) | 90° Included Angle | MultiCam OEM spec 90° ACM folding bit designed for high-speed automated depth-control routing. |
| 000419-02068 | 108° V-Groove Folding Tool | 108° Included Angle | Specialized wide-angle V-fold bit designed for creating spring-back compensated 90° folds or open-angle architectural fascia panels (up to 72° inside angle / 108° cut profile). |
Technical Parameters for ACM Folding Cutters
-
Flat Tip Landing Width: Typically ground to 0.090" – 0.125" (2.3 mm – 3.2 mm) flat bottom. This ensures the fold forms smoothly along a flat, controlled radius rather than a sharp point, which prevents outer skin metal tearing.
-
Cut Depth Setting (Critical): On standard 3 mm or 4 mm ACM, set the total cut depth to leave 0.012" – 0.016" (0.3 mm – 0.4 mm) of core material on top of the bottom aluminum skin.
-
Operating RPM & Feed Rate:
-
Spindle Speed: 16,000 – 18,000 RPM
-
Feed Rate: 120 – 180 IPM (3.0 m/min – 4.5 m/min)
-
Passes: Single-pass cut for best accuracy and thermal efficiency.
-
Best Practices for MultiCam ACM Folding Setup
-
Calibrate Z-Zero accurately: Use a digital touch plate or pressure-sensitive tool setter to establish precise spoilboard zero, as a variance of even 0.1 mm can result in either skin tearing or insufficient bend depth.
-
Vacuum Hold-Down: Ensure localized high-flow vacuum hold-down to prevent sheet bowing under the vertical pressure of the V-groove tool profile.
-
Chip Removal: Direct compressed air toward the cut path to keep molten plastic core debris from packing into the V-groove tip.
© 2026 Shenzhen Oyea Machinery Co., Ltd. All Rights Reserved 


Call us now!